
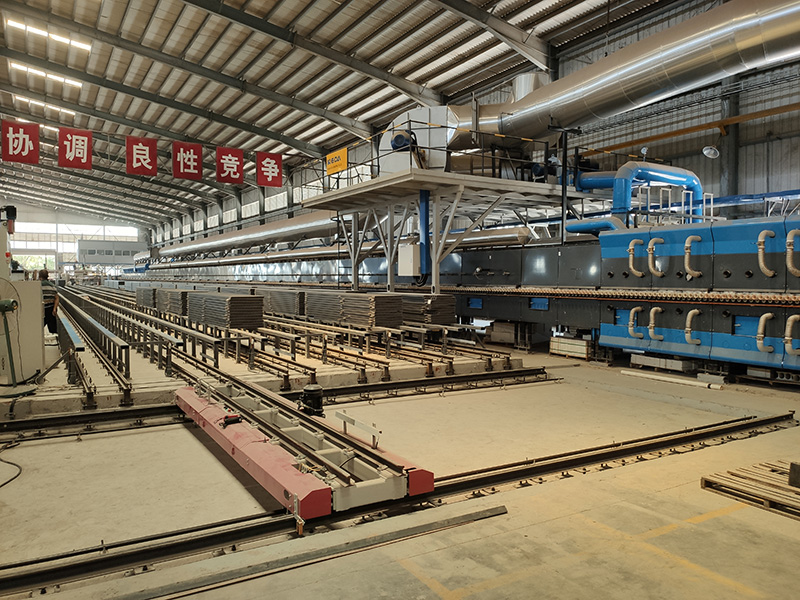
The LOPO third production line is documented here as a dated company archive, not as a current capacity reservation or automatic product approval. LOPO’s company timeline says the third line began operation in 2022; this WordPress record followed on 4 March 2023 with factory photographs and production claims.
For a live order, verify the legal entity and site, current line identity, exact product-to-line route, manufacturable range, trial samples, capacity basis, quality plan, traceability, programme and evidence. A line announcement or factory photograph cannot prove delivered-product quality or complete facade performance.
- Photo metadata
- 14 July 2022 capture timestamps; not commissioning proof
- Company timeline
- Third line reported operating in 2022
- Article date
- 4 March 2023
- Current decision
- Reconfirm product, line, evidence and order-specific availability
Read the archive as dated first-party statements
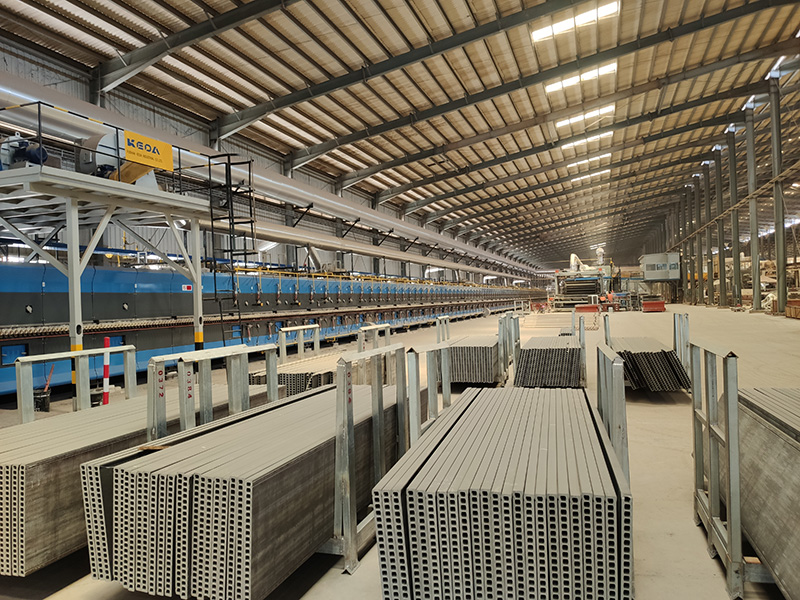
Three LOPO records provide different snapshots. The current company History page records that the third line began operation in 2022 and associates it with an extra-long 3,600 mm terracotta tile. The March 2023 post called the line 300 m long, stated output of up to 2,500 m²/day and described “3D inkjet” plus cutting, gluing and drying equipment. A later 12 January 2026 company factory overview described three approximately 300 m panel lines and company-stated annual capacity up to 2 million m².
These figures are not independent audits, and they use different dates and capacity bases. Do not multiply the daily figure into annual output, combine it with the 2026 figure or treat either as capacity reserved for a project. The legacy global-length superlative has no defined peer set or source and is omitted. The 3,600 mm historical item does not establish a current standard range or suitability for a proposed profile.
| Record | Company-reported statement | Boundary for a current project |
|---|---|---|
| 2022 timeline milestone | Third production line began operation; extra-long 3,600 mm terracotta tile introduced | Historic company milestone only; request current line/product drawings, limits, samples and tests |
| 2023 WordPress article | 300 m line; output up to 2,500 m²/day; “3D inkjet” including side patterns; named cutting/gluing/drying functions | Archive claims without model, product mix, method, yield, uptime, evidence or current-status documentation |
| 2026 company overview | Three approximately 300 m professional panel lines; annual capacity up to 2 million m² | Later first-party description, not independent audit, order allocation or proof every product can run on every line |
Define “3D inkjet” before specifying the finish
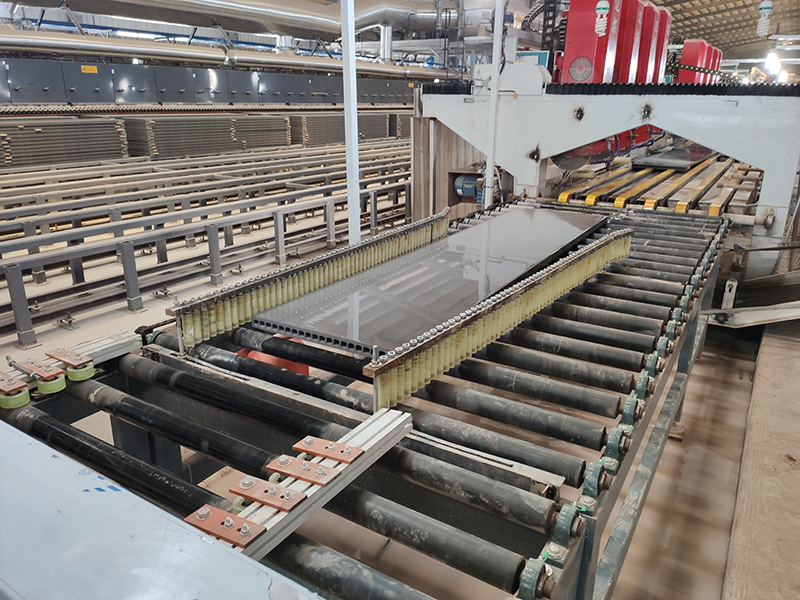
Ask what “3D” means for the proposed product. It may be an archive name for digital decoration, multi-pass tonal depth, surface/edge coverage or another process; it must not be assumed to create three-dimensional geometry. Define the printable face and sides, registration, pattern scale and repeat, orientation, edge/return coverage, body/ground coat/ink/glaze relationship, firing route and the difference between a factory sample and production output.
Exact product
Record item or custom reference, body/profile, dimensions/tolerances, finish build-up, intended use, plant, line and revision.
Digital artwork
Control source file, colour target, scale, repeat, orientation, approved edits, version and release authority.
Face and sides
Identify which surfaces are intentionally printed or treated and how cuts, corners, returns, holes and exposed body should appear.
Sample range
Use signed master and boundary samples for colour, texture, gloss, pattern alignment, print defects, edges and batch variation.
Production control
Link line, recipe/process revision, ink/glaze lots, firing run, inspection records, nonconformances and retained samples.
Use evidence
Match relevant appearance, surface, exposure, cleaning and complete-system evidence to the exact production configuration.
A printed stone-, wood- or metal-like surface does not inherit the source material’s chemistry or performance. Website images cannot control colour, sheen or repeat, and successful sample printing does not approve full-scale yield, edges, installation support, weathering, cleaning or the complete wall.
Qualify the product-to-line route
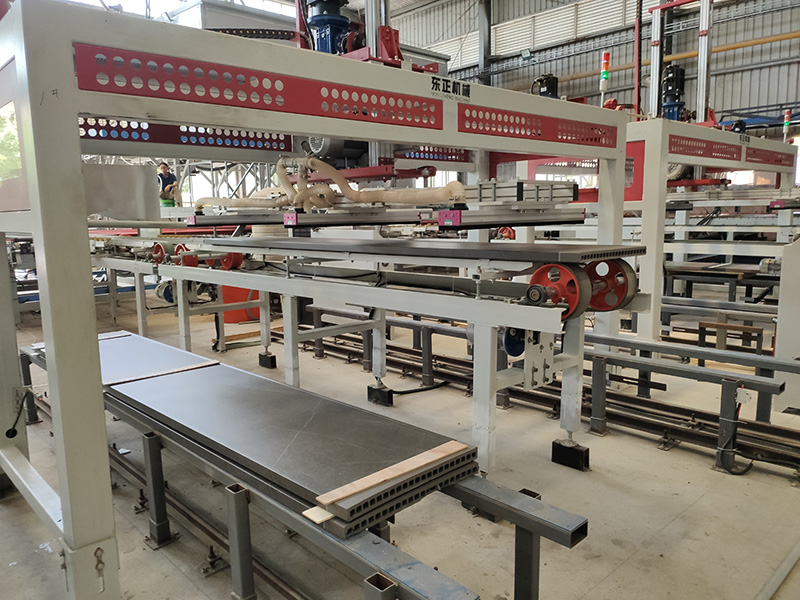
A factory can operate several lines while only one route is appropriate for a given body, profile, finish or special process. Request a flow diagram from approved raw material and forming through drying, surface application, firing, cutting/secondary work, inspection, packing and release. Identify steps that occur on the announced line and steps performed elsewhere, including subcontracted work.
Identify
Confirm contracting and manufacturing entities, site/address, line ID, operating status and the exact quoted product/revision.
Map
Map every production, inspection, secondary-processing and packing step with equipment/site ownership and handoffs.
Trial
Run representative formats, finish, edges and quantities; review range, defects, tolerances, handling and repeatability against agreed criteria.
Release
Approve product and quality plans, evidence, capacity/programme basis, traceability, change control, nonconformance and shipment records.
Do not infer manufacturable size from the apparent panel stacks or machine opening in a photograph. The current line envelope must cover face length/width, profile and cavities, thickness, mass, straightness/flatness, finish and edge requirements, tolerances, special units and packing. Confirm where cuts, grooves, drilling or other secondary work occur and whether those operations affect support zones, edges or test applicability.
Ask what a capacity number includes
Capacity may mean nameplate/theoretical output, a best shift, demonstrated sustained production, saleable output after yield loss, annual output across a product mix or capacity currently available after committed orders. Require the unit, product/profile/finish, shift pattern, operating days, utilization, yield basis, bottleneck and reporting period. Do not convert length or speed into saleable square metres without a declared model.
| Input | Question | Required project record |
|---|---|---|
| Product mix | Which profiles, sizes, finishes, colours and specials share forming, printing, kiln, cutting and packing resources? | Quoted routing and planning assumptions for the exact schedule |
| Rated vs saleable output | Is the figure theoretical, demonstrated, gross, good-output or shipment-ready? | Defined unit/period, product basis, utilization/yield and source date |
| Bottleneck | Which step controls output for the proposed configuration? | Line/step plan covering trials, surface work, firing, secondary work, inspection and packing |
| Changeover and holds | How do recipe, profile, colour/finish, maintenance, testing and QA releases affect sequence? | Order-specific production schedule with realistic changeover and hold points |
| Committed load | What capacity is already allocated and what contingency exists for downtime, rework or retest? | Dated allocation statement and recovery/escalation plan |
| Logistics | Can crating, storage, container/loading, transport and site call-offs keep pace without damaging traceability? | Packing/shipping plan linked to batches, elevations and delivery dates |
Daily and annual company figures may serve as prequalification inputs, but the contract programme must be based on the proposed product mix and allocated slot. Separate manufacturing completion from inspection release, packing, shipment, customs, inland delivery and site availability.
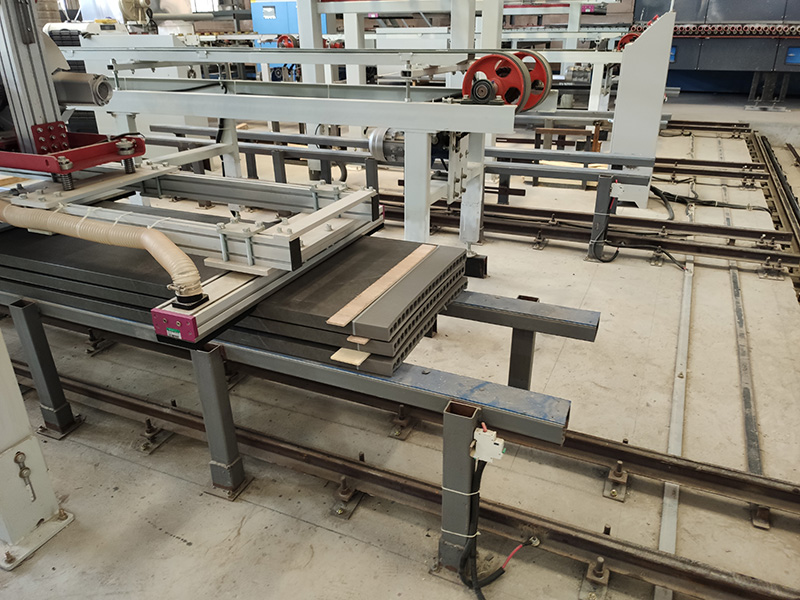
Connect factory evidence to the delivered batch
- contracting entity, manufacturing entity, address, line ID/status, quality-system scope and named project contacts;
- current product drawings, intended use, production route, manufacturable envelope, sample/finish range and product/assembly reports;
- inspection and test plan with incoming, in-process, final, packing and pre-shipment hold points and acceptance criteria;
- traceability from raw-material/body and surface lots through forming, drying, printing/glazing, firing, secondary work, inspection, crate and elevation;
- equipment calibration/verification and maintenance records where they affect the specified characteristics;
- trial and mock-up results, approved masters/boundaries, production control samples and retained replacement samples;
- nonconformance, concession, repair, segregation, reinspection/retest and change-control procedures; and
- order-specific capacity allocation, production/packing/shipping programme, contingency, progress reporting and release records.
Employment, local-economic and environmental claims in the old article were not supported by job counts, workforce records, permits, audited emissions/waste/energy data or a scoped product declaration, so they are not repeated as outcomes. Where these issues are material to procurement, request current site- and period-specific documents, identify the responsible entity and distinguish regulatory compliance from comparative environmental performance.
At handover, retain approved samples, product/finish revisions, line and batch records, calculations/tests, inspections, deviations, packing/shipping records, as-built locations, cleaning/maintenance information and labelled spares. A photograph of a line is useful history; project confidence comes from a traceable chain between the quoted product, controlled manufacture, accepted evidence and delivered units.
Verify the line against an exact terracotta schedule
Share product type, profile and dimensions, finish/inkjet intent, quantities, special pieces, performance requirements, sample/mock-up stages, quality hold points, packing/delivery destination and programme. Request a current product-to-line route, evidence list and order-specific capacity statement.