
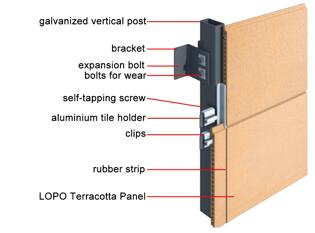
Terracotta facade installation quality-control guide
A reliable inspection result starts with defined project requirements, competent people, controlled materials, calibrated measurement and traceable records—not a universal percentage. This guide preserves the 2019 “non-beam dry-hanging” defect archive and its three original images while replacing unsupported pass-rate claims and prescriptive site instructions with project-specific hold points and responsibility boundaries.

Why the old percentages are not acceptance criteria
The 2019 page printed several defect or pass figures without a report, project, inspected population, sampling method, unit of measure, date, acceptance rule or calculation. They remain traceable below as source artefacts, not benchmarks.
| Printed value | Old description | Evidence treatment |
|---|---|---|
| 71.55% | Uneven surface and joints not flat. | No denominator or measurement rule; not a universal failure rate. |
5077% | Connector “not qualified.” | Invalid as printed. It may contain a missing decimal, but the source cannot support a correction. |
| 30.77% | Terracotta panel installation “unqualified.” | No lot, sample or definition of a nonconforming installation. |
| 95% | Inspection pass-rate target in the title. | No baseline study or project approval; not an acceptable substitute for meeting every mandatory criterion. |
| 100% | Old instruction associated with laser-theodolite checking before “full soldering.” | The characteristic, tolerance and population are undefined; the phrase does not approve a weld sequence. |
A meaningful quality metric identifies the inspection lot, characteristic, approved tolerance, instrument and calibration status, sampling or full-inspection rule, numerator, denominator, stage, date, inspector and disposition of every nonconformance. A high aggregate pass percentage cannot waive a safety-critical defect or an unmet mandatory requirement.
Start with the project quality plan and responsibilities
Before procurement or installation, align the issued design, specification, approved product/system data, calculations, applicable codes and standards, authority requirements, inspection and test plan, method statements, drawings, samples and mock-up criteria. Record revisions and resolve conflicts through the designated design authority.
Design team
Defines performance, design actions, supports, anchors, movement, interfaces, cavity/fire and water strategy, tolerances, inspection criteria and delegated-design limits.
Supplier
Provides identified product data, batches, dimensions, declared tolerances, handling limits and scoped evidence; it does not approve the building substrate or installer’s system.
Contractor and installer
Submit procedures, competent-person records, equipment and calibration status, traceability, first-off work, inspections and nonconformance controls.
Inspector / authority
Witnesses defined hold points, checks records and installed work against approved criteria, and tracks unresolved items without assuming design responsibility.
2019 problem types retained as an audit checklist
The old account associated nonconformance with uneven panel planes, irregular joints, misaligned connectors, inaccurate bracket-to-post work, an uneven base wall, unverified measuring instruments, weak incoming-material controls, missing testing, incomplete technical briefing and insufficient personnel training. It also questioned whether clips had an intended flexible interface.
Convert those observations into project records: confirm substrate survey and release; approved set-out datums; installer competence; incoming inspection; component identity and condition; instrument calibration; connector and support positions; panel alignment and joints; interface components; coating repair; and closed nonconformance reports. Do not copy the old corrective wording without design approval.
Control points from receipt to set-out
“Straight,” “flat” and “vertical” need numeric project tolerances and a stated measurement method. Laser instruments, levels, total stations, tapes, gauges or templates are selected and checked for the required accuracy; their use alone does not create a 100% pass.
Supports, anchors, welding and corrosion protection
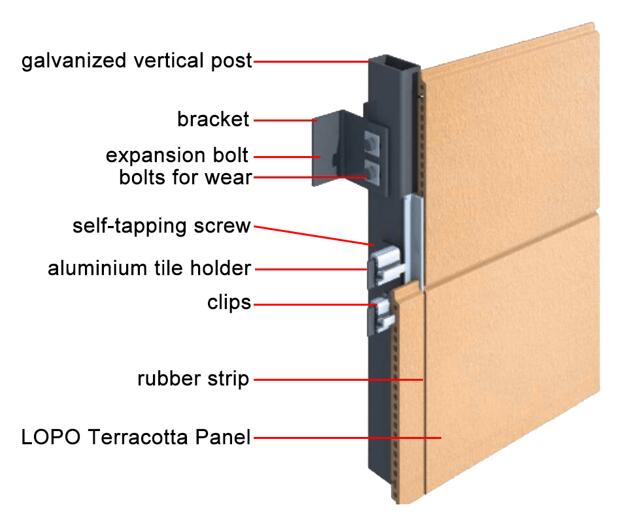
Check support and connector type, material/grade, coating, location, orientation, edge and end conditions, embedment or engagement, adjustment range and tightening/locking against the approved documents. Loads, substrate capacity, anchor selection, spacing, testing and acceptance are determined by the project engineer and applicable approvals—not by the archive diagram.
Verify the specified corrosion-protection system for the actual metals, environment, cut edges, holes, fasteners and weld areas. Surface preparation, coating repair, thickness and inspection follow current project documents and manufacturer data. A generic “anti-rust treatment” is not a complete specification.
Clips, pads and material compatibility
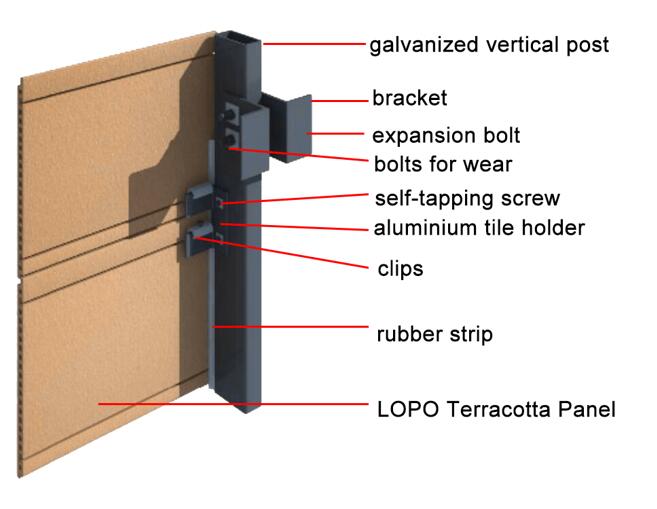
The 2019 text proposed a circular spring piece between panel and clip and a plastic spacer between pendant and bracket. Those historical terms do not authorize either component. The approved design must identify the clip, holder, pad, isolator or spring element; its material, geometry, position, retention and replacement; and its compatibility with the terracotta, metals, coatings, design movement and exposure.
Project review should address load transfer and retention, bearing/contact pressure, tolerance take-up, creep or compression set, temperature and moisture exposure, ageing, galvanic contact, fire/cavity requirements, drainage and water control, installation damage and inspectability. Required evidence and acceptance belong to the complete identified assembly.
Mock-up, staged inspection and nonconformance closure
Use approved samples and a representative mock-up to agree appearance, panel range, joints, corners, openings, transitions, interfaces, access and workmanship before repetitive installation. Record what the mock-up does and does not approve; retain the accepted reference under controlled conditions.
Plan inspections at receipt, substrate release, set-out, first-off support work, concealed components, first panel area, defined production lots and completion. Safety-critical or concealed work may require witness or hold points and project-defined inspection or testing frequency.
Trend recurring defects by defined category and denominator to guide corrective action. Report both open and closed items; an overall pass percentage must not conceal unresolved, repeated or safety-critical nonconformance.
Minimum traceable record set
Retain issued documents and revisions, design responsibility matrix, calculations and approvals, product/system identification, incoming inspection, batch records, storage checks, instrument calibration/verification, survey and set-out, substrate release, installer and welder competence where relevant, approved procedures, first-off and mock-up approvals, anchor/connection/weld/coating inspection required by the project, concealed-work records, panel/joint inspections, test reports, photographs, nonconformance and repair approvals, reinspection and handover/as-built information.
Prepare a project-specific quality brief
Send the project location, elevations, identified panel/system, substrate and support concept, applicable standards and authority requirements, design criteria, drawings, inspection/test plan, mock-up scope, preliminary quantities, programme and responsible engineering contacts. Request current scoped product and system documents; final design, installation and acceptance remain with the project team.