
A 3D inkjet terracotta facade combines a fired-clay panel body with a digitally developed surface pattern. It can introduce fine mineral movement, marble-like veining or other controlled imagery while retaining the module and fixing logic of a terracotta rainscreen.
PG235 is an archived LOPO reference shown with a light stone-like finish. The historic specification remains useful for orientation, but the offered panel, print, dimensions, test documents, minimum quantity and programme must be confirmed for each current project.

Separate the clay body from the printed appearance
The panel body and its decorative face perform different roles. Extruded and fired clay establishes the section, hollows, edges and fixing interfaces. Digital decoration establishes the visible pattern and colour. A project should review both, including what happens at cut edges, grooves, corners and any exposed panel ends.
Body
Confirm clay reference, section drawing, dimensions, tolerances, mass and fixing zones.
Surface
Approve print family, scale, direction, gloss, texture and acceptable colour range.
Assembly
Coordinate clips, rails, cavity, insulation, membranes, flashings and fire stopping.
A stone image should be judged as its own ceramic finish. It need not copy a named quarry exactly, and a photograph cannot establish the approved colour or long-term performance.
Use the PG235 archive without treating it as current data
| Archived field | 2016 value | Current confirmation |
|---|---|---|
| Item and size | PG235; customized | Available tooling, panel schedule and manufacturing limits |
| Material and thickness | Natural clay; 18 mm | Exact offered section, reference and dimensional tolerances |
| Colour and finish | Mix; 3D inkjet | Physical samples, print layout and approved visual range |
| Archived mass | 31 kg/m² | Mass for the exact panel size, body and finish |
| Water absorption | Less than 0.5% | Applicable current test method, report and product scope |
| Commercial notes | MOQ 1500 m²; lead time 35 days | Current quotation, production review and delivery schedule |
Specification boundary: product codes and archived values can change. Do not extend an old result to a new size, print, fixing or market without a current technical review.
Control pattern scale, repetition and variation
Stone contains non-repeating movement, whereas digital printing begins with artwork and a production sequence. Ask how many pattern variations are available, whether panels have a preferred orientation and how the layout avoids obvious repeats across broad elevations.
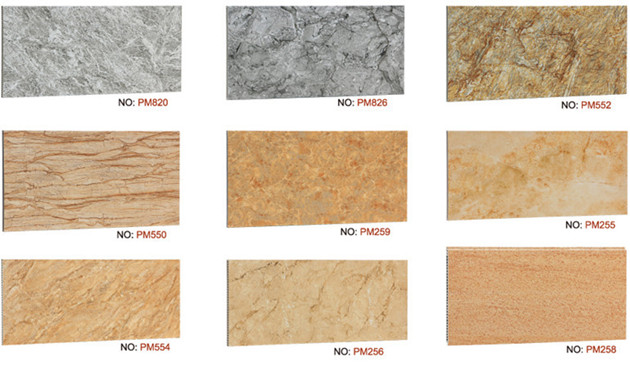
Build a multi-panel mock-up with the proposed joints and corner treatment. Review it from close and distant viewpoints in project light. Record panel orientation and any deliberate mix so production labels and site installation can follow the approved composition.
Compare ceramic and stone on project evidence
Printed terracotta and natural stone are not interchangeable versions of one material. Each has its own appearance, thickness, fixing, tolerances, test route, maintenance and cost structure. Select between them using the actual wall design and project priorities rather than a general claim that one is always superior.
If environmental performance matters, request product-specific information and compare defined life-cycle boundaries. “Natural clay” alone does not establish a lower impact, just as a stone-like print does not provide the properties of quarried stone.
Detail the complete ventilated facade
The terracotta panel sheds most direct rain, while the cavity drains incidental water and allows ventilation. The backup wall, air and water barriers, insulation and flashings complete the envelope. Coordinate cavity openings, fire barriers and drainage paths so every layer remains continuous at windows, parapets, bases and material transitions.
The facade engineer should verify wind loads, panel spans, clips, rails, brackets, anchors, movement and replacement access. Construction tolerances must be absorbed in adjustable supports without forcing or over-constraining the ceramic panels.
Choose applications through technical review
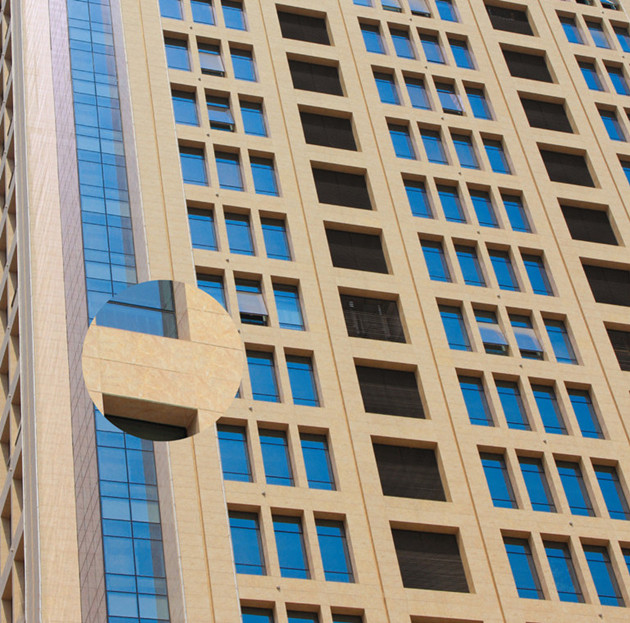
3D inkjet terracotta can be considered for new or renovated exterior walls, commercial podiums, public buildings and selected interior feature walls. Transport stations, tunnels and overhead locations introduce additional impact, restraint, fire, access and maintenance requirements that must be resolved by the responsible team.
The old listing mentioned clinical clean rooms and food-production spaces. A facade panel should not be assumed hygienic or suitable for controlled environments without evidence for joints, cleanability, emissions, contamination control and the local approval route.
Approve samples and preserve the design through delivery
Issue an elevation schedule with panel sizes, pattern orientation, cuts and specials. Approve representative samples and a mock-up before bulk manufacture. Define inspection criteria for dimensions, surface, colour, edges and identification, then coordinate packing by elevation or installation zone.
- approved panel reference, section, finish range and mock-up;
- current reports, system drawings, calculations and interface details;
- production, inspection, crate and installation-zone schedules;
- cleaning guidance, replacement method and labelled spare panels.
On site, check the subframe and datums before installation. Establish a benchmark area for joints, print distribution and corners, protect completed surfaces and trial any cleaning method on a discreet location.
Discuss a 3D inkjet terracotta facade
Send the project country, elevations, facade area, target stone or mineral direction, panel sizes, fixing concept, required standards, quantity and programme. LOPO can review PG235 or current terracotta rainscreen alternatives, sample development and manufacturing feasibility.