
Light-colored decorative terracotta panels offer a pale facade palette while retaining the module, depth and fired surface of architectural ceramics. Digital inkjet decoration can introduce marble-like veining or other designed patterns, but a successful specification must coordinate the image with ceramic manufacture, panel layout, fixing and long-term exposure.
PM880 appeared in LOPO’s 2016 archive as a customized, light marble-look panel. Historical dimensions, performance figures, minimum order and lead time are retained below for context; every value should be confirmed against a current project-specific product sheet before design or purchase.

Understand the printed ceramic surface
Digital inkjet equipment applies a controlled graphic to the ceramic surface before the final firing sequence is complete. The process can reproduce a designed pattern across multiple units and can create stone-, wood- or abstract-inspired effects. The substrate remains a fired-clay or ceramic panel; the printed appearance does not make it natural stone.
Printer resolution and droplet specifications were prominent in the original marketing language, but they do not by themselves predict facade quality. The result also depends on artwork preparation, ink and surface compatibility, glaze or protective layer where used, firing, color calibration and how the graphic is divided across the panel grid. Approve the finished ceramic, not the printer specification.
Design a light palette rather than a stone imitation
Light panels can reduce the visual weight of a large wall and pair readily with glass, dark metal, timber tones or natural clay accents. A marble reference may guide veining and contrast, but the facade should be composed around ceramic modules. Repeating an identical graphic can reveal obvious tiles; uncontrolled rotation can interrupt veins at joints.
Base tone
Approve the pale background against adjacent sealants, metal finishes, glazing and soffits in project lighting.
Pattern scale
Set vein width and frequency for the actual viewing distance instead of enlarging a small sample indiscriminately.
Panel sequence
Decide whether graphics repeat, rotate or flow across several modules, and provide an installation map where needed.
A physical layout of several panels is more useful than a single beauty sample. It exposes repeating motifs, edge transitions, joint interruption and the combined color range before production expands.
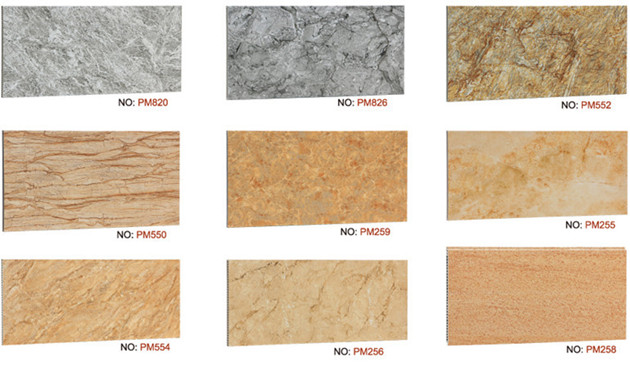
Read the archived PM880 specification carefully
| Archived 2016 field | Archived value | Current action |
|---|---|---|
| Item / material | PM880 / natural clay | Confirm current product name, body and manufacturing plant |
| Size / thickness | Customized / 18 mm | Verify feasible module, section, tolerances and fixing compatibility |
| Color / finish | Mix / 3D inkjet | Approve current fired range and multi-panel pattern layout |
| Nominal weight | 31 kg/m² | Use current declared mass and actual module for structural design |
| Water absorption | Less than 0.5% | Request the applicable current test report and product identification |
| MOQ / lead time | 1,500 m² / 35 days | Reconfirm against quantity, samples, testing, finish and schedule |
The old values should not be copied into a tender as guarantees. Custom dimensions can change weight, span, support and yield; custom graphics add artwork and sampling stages. Allow time for feasibility review, sample firing, approval, testing where required and production.
Detail the panel as part of a rainscreen
For an exterior ventilated facade, coordinate panel section and support with the subframe, brackets, insulation, cavity barriers, flashings and water-management layers. Draw window heads, jambs and sills, parapets, base conditions, corners and transitions to other materials. Pale surfaces make inconsistent joints and poorly aligned closures especially visible.
The facade engineer must verify design actions, panel span, fixings, movement, impact exposure and applicable codes for the complete assembly. A printed decorative surface does not establish structural or fire performance. Use current test evidence tied to the proposed product and system.
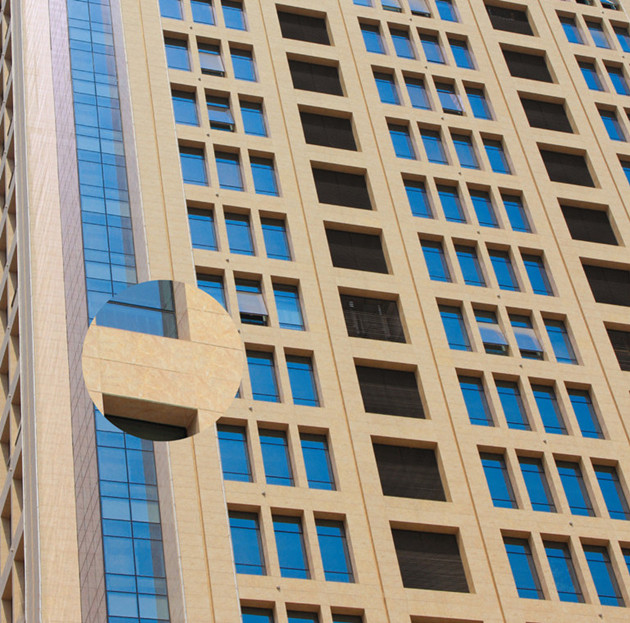
Match the application to verified performance
The original page proposed a broad list of settings, from exterior walls and transport spaces to ceilings and hygiene-sensitive rooms. Not every printed panel or fixing system is appropriate for every location. Underground areas may add impact, moisture and cleaning demands; ceilings require overhead-retention design; clean rooms and food or medical environments require documented surface, joint and cleaning compatibility.
Define the application first, then request relevant current documentation. Compare printed panels with naturally colored terracotta rainscreen panels and other architectural terracotta products before selecting the finish route.
Approve samples, mock-ups and maintenance
Use a staged review: artwork proof, fired single panel, multi-panel layout and representative wall mock-up. The mock-up should contain the actual joint, subframe and at least one corner or opening. Review color, gloss, pattern repetition, alignment and cleaning in direct and raking light.
Agree acceptable appearance and replacement rules, retain signed samples, and order labeled spares covering the approved color range. Cleaning trials should use the proposed method on a spare panel; avoid assuming that a process suitable for natural stone or unprinted terracotta is automatically suitable for an inkjet-decorated ceramic surface.
Selection principle: specify PM880—or a current successor—by approved fired appearance, identified product and verified assembly performance, not by an archived image or generic marble description.
Request current light-colored panel samples
Send the project location, elevations, target module, light-color or marble reference, estimated quantity, required performance, fixing concept and schedule. LOPO can review current product availability and prepare relevant fired samples and profile information for the project team’s evaluation.